
What Is Chemical Manufacturing Asset Management Software?
Chemical Manufacturing Asset Management Software is a system that holds one live record for every physical asset on your site, including reactors, pressure vessels, pumps, heat exchangers, storage tanks, and local exhaust ventilation (LEV). Each record carries the asset’s condition, maintenance history, inspection due dates, and statutory paperwork.
On most sites, that information is split across a plant equipment list, paper written schemes, and a maintenance spreadsheet. The software pulls it into a single asset register, usually keyed to the tag numbers on your piping and instrumentation diagrams (P&IDs). An engineer on the unit and a manager preparing for an audit then work from the same data.
The use of chemical manufacturing software tools, such as Asset Management Software is welcomed in an industry that relies heavily on the upkeep of its assets and production plant.
Why Asset Management Is Essential in Chemical Manufacturing
Asset management is essential in chemical manufacturing because the condition of your equipment decides whether hazardous substances stay contained, and UK regulations expect you to prove you are controlling that condition. Weak asset records expose you on four fronts: compliance, process safety, legal liability, and lost production.
UK Regulations Require an Equipment Inventory and a Condition Strategy
If your site is a Control of Major Accident Hazards (COMAH) establishment, your safety management system must cover the “management and control of the risks associated with ageing equipment installed in the establishment and its corrosion”. It must also include an “inventory of the establishment’s equipment, and the strategy and methodology for the monitoring and control of the condition” of that equipment. In software terms, that is an asset register and a maintenance strategy, written into law.
Once you have dozens of pressure systems, LEV units, and hazardous-area items on one site, a spreadsheet stops being a dependable way to know what is overdue. Asset Management Software schedules each regime against the right asset and shows you the gaps before an inspector does.
Ageing Chemical Plant Drives a Large Share of Major Hazard Incidents
HSE guidance on ageing plant reports that around 60% of major hazard loss of containment incidents relate to technical integrity, and half of those have ageing as a contributory factor. Between 1980 and 2006, 96 major accident loss of containment incidents in the EU’s Major Accident Reporting System (MARS) were primarily caused by ageing plant mechanisms. That is 30% of all major accident loss of containment events reported.
Software will not stop corrosion. It does keep thickness readings, inspection findings, and overdue remedial actions attached to the asset, where someone is accountable for acting on them.
Missing Maintenance Records Weaken Your Legal Defence
In August 2025, Dundas Chemical Company (Mosspark) Limited was fined £100,000 after a worker suffered burns at its Omoa Works site in Newarthill, Motherwell. HSE found that the mixing valve supplying hot water for cleaning was not maintained in efficient working order or in good repair. The company told HSE there were no records associated with the maintenance of the valve, hose, or nozzle.
A maintenance history held against each asset gives you evidence of what was inspected, what was found, and what was done about it. Without that history, you have nothing to show a regulator or a court.
Unplanned Downtime Erodes Chemical Manufacturing Margins
Siemens’ The True Cost of Downtime 2024 estimates that the world’s 500 largest companies lose around $1.4 trillion a year to unplanned downtime, equal to 11% of their revenues. The average large plant in the study loses 27 hours a month.
When you assess the cost of asset management software, weigh the subscription against one lost batch or one day of lost output on your site, not against the cost of keeping a spreadsheet.
Key Asset Management Features For Chemical Manufacturing
Feature | The Problem It Solves | What the Software Does |
Asset Register | Equipment data sits across drawings, data sheets, and spreadsheets, so technicians waste time finding specifications and risk fitting parts in the wrong material for the process fluid. | Organises assets as site, unit, system, equipment, and component. Each record carries the P&ID tag number, service, materials of construction, criticality rating, and attached data sheets, drawings, and certificates. |
Statutory Inspection Scheduling (PSSR, LOLER, and LEV) | You run several inspection regimes with different intervals. Pressure systems follow their written scheme, LEV needs a thorough examination at least every 14 months, and LOLER sets six months for lifting accessories and 12 months for other lifting equipment, unless an examination scheme sets different intervals. | Holds each interval against the right asset, raises the job before it falls due, and stores the examiner’s report and any defects on the asset record. Produces one overdue report, filtered by regulation. |
Condition Monitoring and Corrosion Tracking | Corrosion and erosion build up unseen. HSE defines ageing by condition, not age, so you need evidence of how each asset is deteriorating. | Stores thickness, vibration, and other readings against each asset, trends them over time, and alerts you when a reading crosses a threshold you set. Larger systems pull live readings from sensors or a plant historian. |
Risk-Based Inspection (RBI) Support | With hundreds of vessels and pipework circuits, inspecting everything at the same frequency wastes effort on low-risk items. RBI, as defined in API RP 581, prioritises inspection by combining the likelihood and consequence of failure. | Holds risk rankings (natively or from a specialist RBI tool) and uses them to set inspection priorities. Records competent person approval when an interval changes, because pressure system intervals still sit within your written scheme. |
Work Orders Linked to Permit to Work and Isolations | HSE defines a permit to work as “a formal recorded process used to control work which is identified as potentially hazardous”. | Links the work order, permit, isolation, and close-out sign-off on one asset record. Some vendors offer electronic permits natively; others integrate with your existing permit system. HSE guidance sets out what electronic permit systems must do safely. |
Critical Spares Linked to Plant Equipment | A failed mechanical seal on a critical pump can stop a unit if the replacement is not on the shelf. | Links each spare to the equipment it fits, sets minimum stock levels for critical items, and shows every asset a part is used on. The part record carries the same material specification as the asset. |
Mobile Access for Plant Rounds and Hazardous Areas | Technicians log readings and defects at the equipment, often where signal is weak. In zoned areas, the device itself must meet the Equipment and Protective Systems Intended for Use in Potentially Explosive Atmospheres Regulations 2016 and carry the Ex marking. | Provides an offline mobile app that syncs when it reconnects. The vendor does not certify your hardware, so the app must run on the Ex-certified phones or tablets your site already uses. |
Management of Change and Audit Trails | Every change to an asset, from a new relief valve setting to a replaced heat exchanger bundle, needs a record for your COMAH safety management system and your process safety indicators. | Keeps an automatic, locked history of what changed, when, and who approved it. Feeds indicators such as the share of safety-critical inspections completed on time. |
3 Leading Benefits of Chemical Manufacturing Asset Management
1. Improve Reliability of Chemical Assets
Asset management aims to provide chemical manufacturers with a quantifiable return on investment (ROI) from each asset. Whether that be plants, machinery, pumps, extractors, or chemical tanks. To achieve a profitable ROI, assets need to be available and operating at a continuous optimal level.
In a multi-billion pound industry such as chemical engineering, the reliability and upkeep of chemical equipment are essential. But it’s also important to understand that assets – be they equipment or infrastructure – have a pre-determined design life, which affects their performance and operational life. Of the 700 to 800 fixed offshore oil platforms and bridges in the Middle East, 70% exceed their design life of 25 years.
Several factors can affect the reliability of assets:
- Ageing assets
- A lack of preventive maintenance
- The use of harsh and hazardous chemicals
With access to incremental asset data – purchase date, general usage, maintenance history, etc. – engineers and asset managers can determine the best course of action to ensure greater reliability of assets.
On top of that, asset managers can prioritise work orders, manage and automate inventory control, improve safety and compliance throughout a production plant, and build cost-saving maintenance programs.
2. Manage Equipment & Infrastructure Lifecycle
Once the purchase of an asset has been planned and completed, it then begins its operational life within the production line. During this time, an asset management solution will provide the tools necessary to track each asset’s lifecycle.
Typically, in a sophisticated system, data is retrieved through the use of IoT (Internet of Things) devices that work on an automated trigger to measure usage and output. Collected data includes:
- Operational output
- Usage
- Current condition
- Assigned operators
- Work order history
- Maintenance and repair history
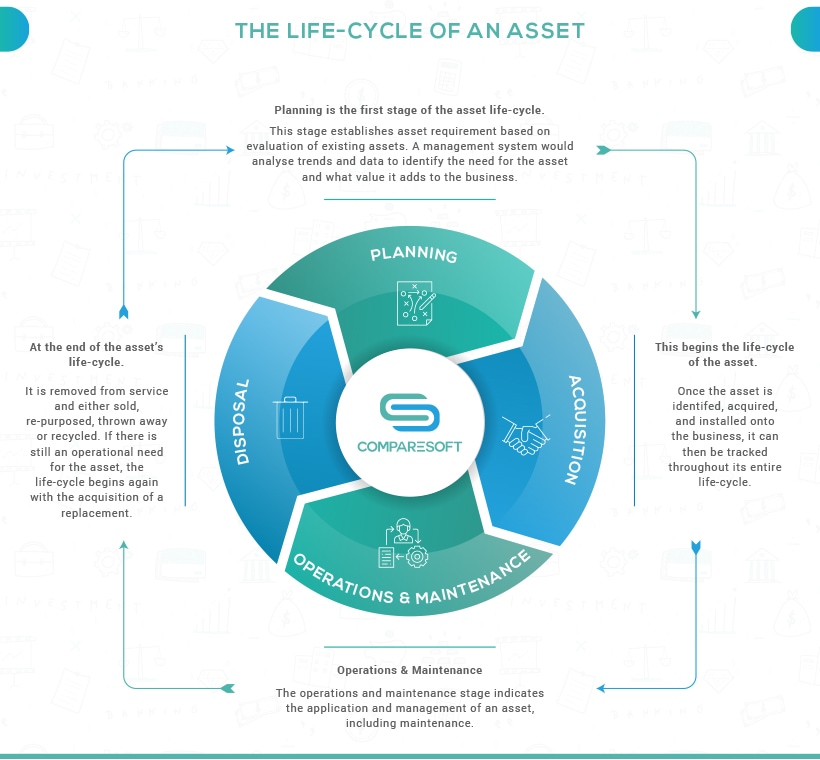
With an overwhelming number of workplace assets, such as machinery and operational components, the ability to track and manage chemical equipment will increase the accuracy and quantity of performance data.
With this data, manufacturers can build proactive asset maintenance programs to decrease asset downtime and determining the value each asset contributes to your overall production output.
For example, if a batch reactor is coming to the end of its useful life, you will have the data to gauge if it’s an essential asset that needs repairing or if its ROI is minimal and needs disposing of.
3. Get a Handle on Operational Costs
Chemical manufacturers will be aware of the ongoing operational costs that affect their bottom line. These come in the form of replacing ageing and deteriorating equipment – caused by heavy and corrosive chemical compounds, excessive unplanned downtime of mission-critical equipment and machinery, and expensive emergency repair costs and technician call-outs.
Asset Management Software has the capabilities that allow manufacturers to better understand their costs:
Automate Asset Purchases
The ordering and procurement of raw materials such as oil, gas, and air can come at a hefty price. That means businesses need to take as much caution as possible with spending to be able to keep profits high.
Asset Management Software enables greater control when it comes to ordering materials, allowing asset managers to calculate the right amount needed to stop over-ordering and needless spending.
The same applies to the ordering of spare parts. Maintenance managers can build a maintenance schedule by collecting real-time performance data. In terms of a chemical plant, engineers will know when a component inside a reactor is wearing down before it fails.
This allows businesses to have a spare part on order, even while a machine is running, to have it at hand when it eventually needs replacing. If the spare part isn’t in stock when the reactor fails, it will incur unplanned downtime.
Through the use of IoT devices, the inventory ordering process can also be automated. By supplying an asset management system with the correct information for ordering spare parts, devices can talk to each other and automatically decide when a part needs ordering. Completely removing human interaction from the process and streamlining inventory purchases.
Reduce Unplanned Downtime
Preventive maintenance programs enable maintenance teams to highlight opportunities for repairs and services while still in operation. By doing so, they’re able to avoid a large maintenance excess when an asset unexpectedly fails. Causing equipment to be out of use and production to come to an unexpected halt.
Bear in mind that maintenance programs can be pricey to implement. For instance, American chemical producers spent more than $1.26 billion on planned maintenance in 2018. But, the cost for unplanned downtime can equate to as much as 2 to 5 times more than that.
Not only can effective asset management provide significant data to automatically alert relevant technicians when equipment is due for maintenance, but it also acts as a central system for storing relevant information for repairs. Such as manuals, previous operating statuses, documentation, and checklists.
This focused approach lets businesses make sure that the right technicians are attending to the right assets. For example, a technician may be more suited to servicing a fixed film reactor as opposed to a batch reactor. So, when a component of that fixed film reactor needs servicing, an asset management system will automatically notify the right technician.
Calculate ROI for Asset Replacement
The cost of replacing assets can be eye-watering. But, if an asset has a high ROI within a manufacturing plant, then businesses will be at ease knowing the expense will level itself out over time.
By collecting data and forecasting reports, stakeholders can calculate the ROI on all assets throughout the workplace. For example, if one reactor is critical for production, businesses will need to repair or replace it when it begins to deteriorate. But, on the other hand, if that reactor has a low ROI and production can continue without it, it can be disposed of.
Asset Management Software can not only help calculate the total cost of ownership and ROI for valuable equipment, but it can apply to materials and employees, too.
Challenges of Managing Assets In the Chemical Industry
There are several challenges that chemical engineering plants encounter daily, including:
- Unplanned downtime of mission-critical assets
- High maintenance and repair costs due to caustic substances
- Safety issues around hazardous chemical inventory
- High turnover of critical assets
- Delays to material and inventory procurement
- The inability to identify and track asset performance
- Limited understanding of an asset’s ROI
With the global sales of chemicals amounting to $3,500 billion in 2011, the demand within the chemical industry for basic, speciality, and consumer commodities is increasing year on year.
This demand puts an extra strain on production lines, employees and work orders, affecting engineers, technicians, operators, and scientists. Not to mention the increasing importance of keeping machinery and equipment in optimal working condition.
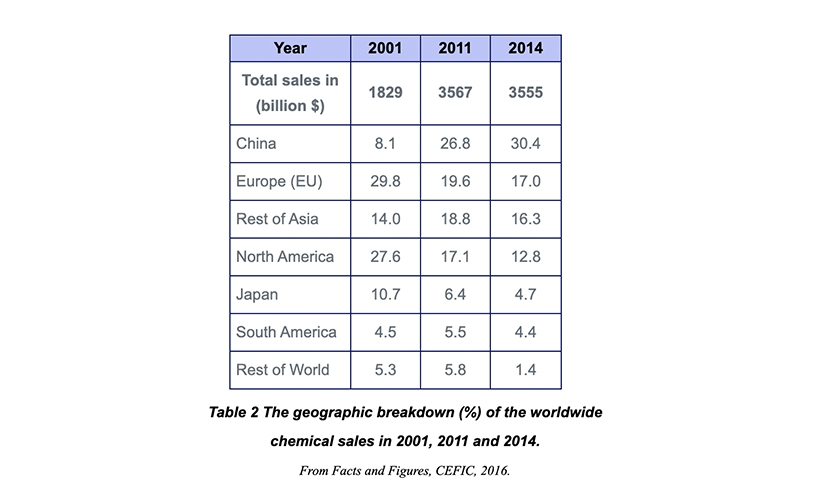
By not ensuring asset reliability during a period of high demand, in which vital chemical equipment and production machinery could fail, businesses experience delays in output along with a damaged reputation. Subsequently, they lose revenue to other chemical manufacturers and miss out on higher profit margins.
The continual expense of maintenance and rising costs of materials have pushed many chemical manufacturers into the process of finding cutting-edge technology to control, maintain, and improve production.